

Personal service
Our service is personal. Mikko, Mikael, and Joni serve our customers directly.
Quick action
In-stock products for export orders are dispatched within 2 business days.
A liquid ring pump is a versatile and reliable solution for pumping clean liquids in industrial processes. Its benefits include self-priming performance, steady flow and the possibility to operate the pump in both directions of rotation. BPI-Chempump’s liquid ring pumps are especially suitable for applications where reliable operation, energy efficiency and trouble-free liquid transfer are valued.
Would you like to send a request for a quote?
Please send us an email or contact us using the form.
Do you have a quick question?
Call or WhatsApp us.
Showing the single result
Liquid ring pumps are an efficient and reliable choice for demanding industrial needs where stability, durability and steady flow are required. Their unique operating principle enables the handling of liquids and gases even in demanding conditions, making them an excellent solution for the chemical industry and water treatment, among others.
A liquid ring pump is based on the vacuum created by a rotating impeller and liquid, enabling efficient transfer of liquids and gases. This operating principle ensures steady flow and makes the pump especially durable. Liquid ring pumps are suitable for a wide range of applications and provide reliable operation even in challenging environments.
BPI-Chempump’s liquid ring pumps offer optimal performance and energy efficiency, making them an ideal choice for various industrial processes. Learn more about the LR-EP liquid ring pump, which is designed for high-quality and long-lasting use.
Steady and trouble-free flow is one of the most important benefits of a liquid ring pump. This feature makes it especially suitable for demanding applications where flow capacity and pressure must remain stable in all conditions. In the chemical industry, for example, the accuracy and reliability of liquid ring pumps are essential when handling sensitive liquids or gases.
Thanks to their energy efficiency and steady performance, liquid ring pumps provide companies with reliable operation and significant cost savings. Lower energy consumption and minimised process disruptions enable more efficient operation and lower maintenance costs. This makes liquid ring pumps a reliable choice for industrial process applications and municipal water treatment systems.
BPI-Chempump’s liquid ring pumps provide an optimal solution for applications that require both efficiency and accuracy. Their ability to operate reliably even in challenging environments and handle a wide range of media ensures consistent quality and performance, whether the application is in chemical industry processes, food production or water distribution systems.
In the chemical industry, the importance of a liquid ring pump is highlighted in processes that require accuracy. Its ability to handle corrosive, volatile or viscous media makes it an ideal choice for environments where material resistance and pressure control are important. A liquid ring pump can handle even aggressive chemicals without reduced performance, which improves process safety and reduces the risk of downtime. In addition, the pumps’ vibration-free operation and steady flow protect sensitive equipment that is often part of chemical industry production chains.
In water treatment, liquid ring pumps are valued for their reliability and wear resistance. These pumps are highly suitable for situations where liquids containing sand, sludge or other solid particles are handled. In municipal water treatment, they provide steady flow, which is essential for maintaining efficient purification processes. This reduces energy consumption and extends the service life of the entire system.
The design of liquid ring pumps enables long-term use without significant maintenance needs. Their closed structure and low wear sensitivity make them a cost-effective solution that meets the needs of both the chemical industry and municipal water treatment plants. When process reliability and continuous operation are critical, liquid ring pumps ensure reliable and efficient performance for years to come.
BPI-Chempump offers high-quality liquid ring pumps designed to meet the needs of demanding industries. Explore our range and find the right solution for your company’s processes. Ask our expert team for more information and request a quote today!
Our staff is always ready to help you choose the right product. If you need more extensive consultation, you can book a free assessment appointment.
"*" indicates required fields
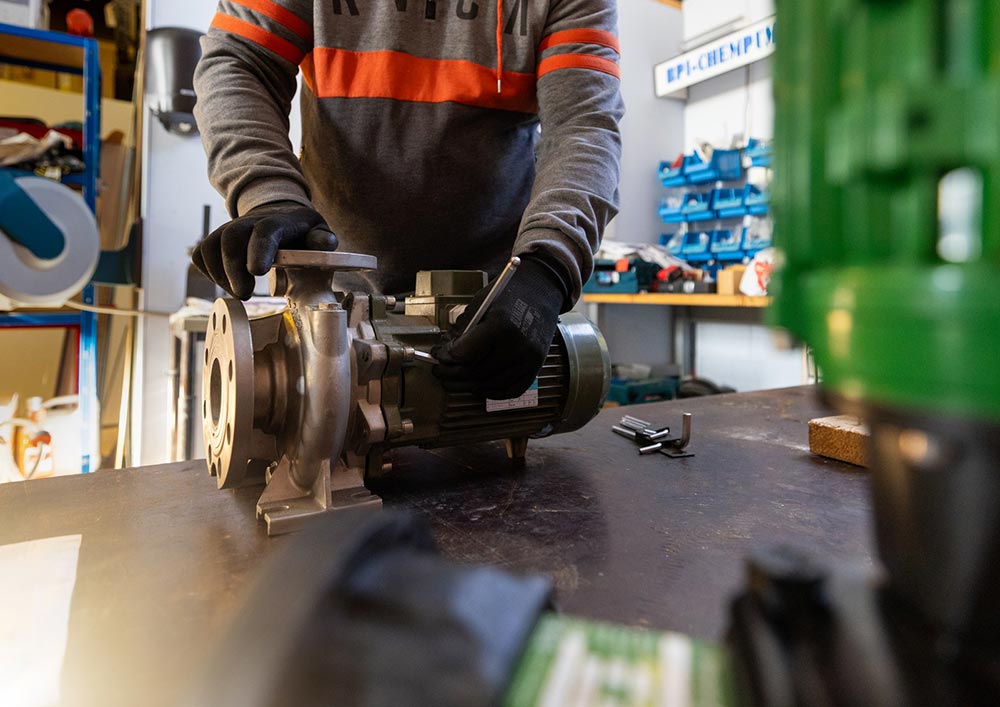
Pump maintenance is a critical part of industrial operations, ensuring that processes continue without interruption and at peak efficiency. BPI‑Chempump specializes in servicing a wide range of pumps to meet the diverse needs of industry.
Regular maintenance helps identify and resolve potential issues before they develop, ensuring continuous and reliable production. Scheduled servicing is the most effective and cost‑efficient way to guarantee the long-term, safe operation of your equipment.
Get in touch with a pump expert, and let’s get your pumps performing at their best!
