

Personal service
Our service is personal. Mikko, Mikael, and Joni serve our customers directly.
Quick action
In-stock products for export orders are dispatched within 2 business days.
A lobe pump is a versatile positive displacement pump suitable for transferring viscous liquids, liquids containing solids and sensitive liquids that require gentle handling. BPI-Chempump’s lobe pumps provide steady flow, high operational reliability and gentle handling for industrial processes, the chemical industry, the food industry and other demanding applications.
Would you like to send a request for a quote?
Please send us an email or contact us using the form.
Do you have a quick question?
Call or WhatsApp us.
Showing the single result
A lobe pump operates using the rotational movement of two synchronised rotors, which transfer liquid efficiently and gently from the suction side to the discharge side. Its unique operating mechanism enables the handling of viscous liquids and liquids containing solids without damage or loss of efficiency. The simple structure, durability and versatile material options make the lobe pump a reliable and long-lasting solution for many industrial needs.
Suction phase: As the rotors rotate, expanding volumes are formed between them at the pump inlet. This creates reduced pressure, or suction, which draws the pumped liquid into the pump. Because the lobes do not touch each other or the pump casing, they can handle viscous liquids and liquids containing solids without risk of damage.
Transfer phase: The pumped liquid remains in the chambers between the rotors. As the rotors continue to rotate, these chambers move towards the pump outlet. The liquid therefore moves steadily without pulsating flow or turbulence, which is especially important when handling sensitive media.
Pressurisation phase: As the rotors rotate, the chambers become smaller at the outlet, forcing the liquid out to the discharge side. In this way, a lobe pump can generate high pressure even at low rotational speed.
Self-priming capability: Lobe pumps are self-priming and can draw liquid from depths of up to eight metres without separate filling or preparation.
Gentle handling: Thanks to its low rotational speed and contact-free operating principle, the pump is gentle on the pumped medium, reducing the risk of damage or changes in composition.
Dry-running resistance: Because the rotors do not touch each other or the casing, a lobe pump can withstand short periods of dry running without damage, which increases operational reliability.
Bidirectional operation: Several models allow operation in both directions of rotation, meaning that the flow direction can be changed when needed.
The Zeilfelder lobe pump has a highly robust structure and is suitable for the needs of many different industries where viscous media, potentially containing solids, need to be handled.
Thanks to the pump’s low rotational speed, the lobe pump is gentle on the pumped liquid. The pumps are self-priming up to eight metres. These pumps also tolerate dry running. Some models also allow operation in both directions of rotation. The Zeilfelder lobe pump is also suitable for ATEX areas and is available for CIP systems when required.
The pump’s simple structure ensures easy maintenance and long service life. Most Zeilfelder lobe pumps have similar bodies, which means that internal components, such as rotors, can be replaced with different types later if needed.
The lobe pump is available with many different material options, and the pump materials are always selected according to the customer’s needs and the application in question. Material options include:
The lobe pump can be equipped with several different shaft sealing options. Seal options include gland packings, lip seals and single or double mechanical shaft seals.
The lobe pump is suitable for handling, among other media:

The pump’s simple and robust structure consists of a body, two rotors and a synchronising gearbox. The synchronising gearbox ensures precise synchronisation between the rotors without contact, which prevents wear and reduces the need for maintenance.
Durable and corrosion-resistant materials, such as stainless steel or acid-resistant stainless steel, are often used. The material selection is always made according to the properties of the pumped medium to ensure the pump’s long service life and safety.
Lobe pumps are versatile devices suitable for a wide range of industrial needs. Their unique operating principle and features make them an excellent choice especially for processes involving viscous, sensitive or solids-containing liquids.
In the food industry, lobe pumps are widely used thanks to their gentle pumping ability. They can transfer sensitive products without breaking their structure, which is important when handling dairy products such as yoghurt, cheese and butter. In the pumping of fruit purées and juices, lobe pumps also preserve product quality without weakening the product’s composition. In chocolate and confectionery production, they enable the accurate and efficient transfer of sugar-rich masses. In the brewery and beverage industry, lobe pumps are essential for handling beer, cider and juice, where both hygienic and gentle pumping are required.
In the chemical industry, the ability of lobe pumps to handle viscous and aggressive media makes them an excellent choice. They can transfer resins, solvents, polymers and other high-viscosity liquids efficiently and safely. The materials of the lobe pump can be selected to withstand corrosion and chemical stress, which expands their use in different chemical processes.
In the oil and gas industry, a lobe pump provides reliability and durability in challenging conditions. They are highly suitable for transferring crude oil and fuels, such as heavy fuel oil. Lobe pumps are also efficient in pumping bitumen and asphalt in construction and road projects. Their ability to handle viscous liquids and liquids containing solids also makes them suitable for sludge handling, such as transferring sludge generated during drilling.
In the agricultural and biotechnology industries, lobe pumps are useful for handling biomass and biowaste, such as in biogas plants where the efficient transfer of organic materials is essential. They are also suitable for accurate dosing of liquid fertilisers and plant protection agents, as well as gentle transfer of enzymes and microorganisms without damage.
Our staff is always ready to help you choose the right product. If you need more extensive consultation, you can book a free assessment appointment.
"*" indicates required fields
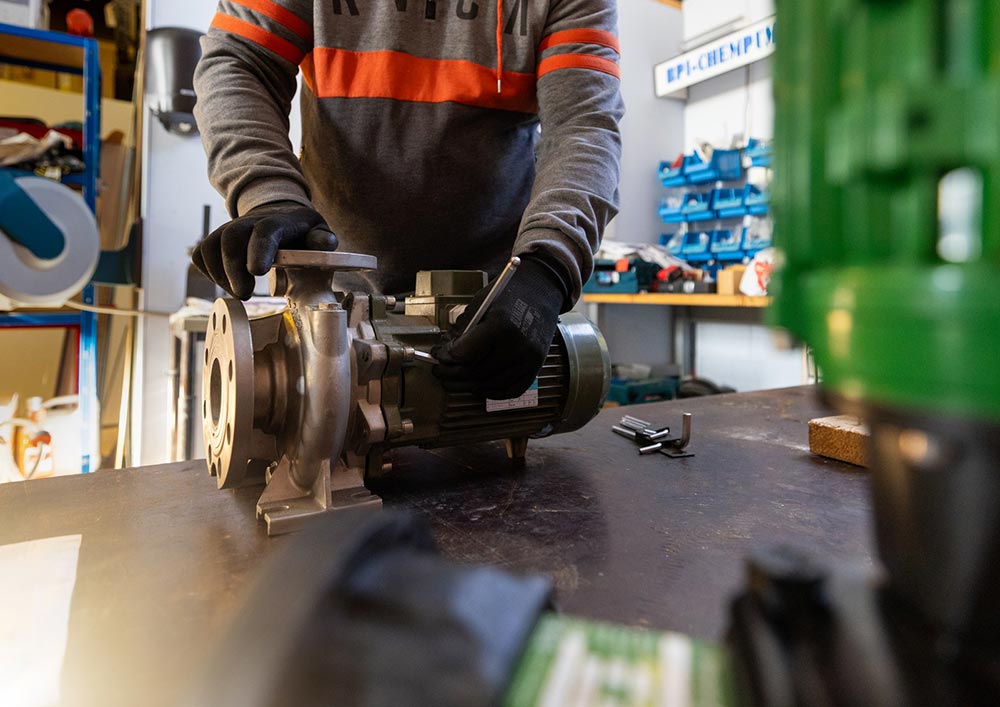
Pump maintenance is a critical part of industrial operations, ensuring that processes continue without interruption and at peak efficiency. BPI‑Chempump specializes in servicing a wide range of pumps to meet the diverse needs of industry.
Regular maintenance helps identify and resolve potential issues before they develop, ensuring continuous and reliable production. Scheduled servicing is the most effective and cost‑efficient way to guarantee the long-term, safe operation of your equipment.
Get in touch with a pump expert, and let’s get your pumps performing at their best!
